Pet Bag Lean Manufacturing: Efficiency for Wholesale Orders
Yes. Lean practice shortens a wholesale pet bag program by removing queue time, not by sewing faster: typical gains are 8-15 percent off the production calendar and 3-6 percent off unit cost. On a 500-piece order quoted at USD 8.90, a 5 percent saving is about USD 225, and a one-week shorter bulk window releases working capital tied up in transit.
Lean is a flow discipline, and for a pet bag buyer its value is calendar predictability more than headline price. Our production team applies pull scheduling, standard work and line balancing to the styles we run repeatedly, which is why repeat reorders behave differently from first orders: material is booked against a released plan, cutting is sequenced by colourway, and packing is sized before the cartons are ordered. Commercial terms remain the reference points you plan around - MOQ 500 pieces per colour, samples in 6-10 working days, bulk production 35-50 days, and final inspection at AQL 2.5. The SGS-verified production base works to ISO 9001 procedures, and lean tools sit inside that system rather than replacing it, so a change in method is a controlled change with a record. Buyers benefit most by asking for flow evidence rather than promises: lead time variance in days, on-time-in-full by order, and work-in-progress levels during peak season. Those three numbers tell you whether a supplier is genuinely levelling its load or simply quoting an optimistic date.
Choosing a pet carrier supplier or a pet bag supplier comes down to the same three checks: a named production base, a test file that matches the destination market, and a price list that states what is excluded. An own-brand launch usually fails on the second check rather than the first, because the file gets assembled after the order instead of before it.
Lean Thinking Applied to Wholesale Pet Bag Programs
Lean started as a production philosophy and became, in practice, a way of describing where time goes. For a wholesale pet bag order, the useful question is not how long each operation takes but how long a unit waits between operations. In many programs the actual sewing, printing and assembly content is a small fraction of the total calendar; the rest is queue, transport, approval and rework loops. Lean work attacks the waiting.
That distinction matters commercially because buyers negotiate the calendar, not the operations. A 35-50 day bulk window is mostly bookable time - fabric arrival, trim arrival, cutting slot, line slot, packing slot - and each slot has a queue behind it. A supplier that levels its load and books slots against a released plan can promise a shorter, more reliable window than one that pushes each order through a first-come queue.
Lean also reframes the minimum order quantity. MOQ 500 exists because set-up and changeover consume line capacity; reduce the changeover and the economic lot size falls with it. Buyers who understand this can negotiate quantity flexibility rather than only price, which is often worth more than a two percent discount when demand is uncertain.
Finally, lean provides a shared vocabulary. When a buyer asks for standard work, a pull signal or a value stream map, a supplier with real lean practice responds with documents and numbers. That shared vocabulary shortens the qualification phase of a sourcing relationship considerably.
The Eight Wastes Visible in a Pet Bag Supply Chain
The classic waste list - overproduction, waiting, transport, over-processing, inventory, motion, defects and unused talent - maps cleanly onto pet bag sourcing. Overproduction shows up as a supplier running a popular colourway ahead of orders and then discounting it; that inventory risk eventually lands in your price. Waiting shows up as a bulk order sitting for days because one trim item has not arrived from a sub-supplier.
Transport and motion wastes are less visible but real. Moving cut panels between buildings, re-handling cartons because the packing plan changed, or walking to a shared hardware store all add minutes that never appear on a quotation. Over-processing is the waste buyers most often create themselves: a specification calling for a tolerance or a finish the market will not pay for, which adds an operation and a failure mode.
| Waste type | Where it appears in pet bag supply | Buyer-visible symptom | Countermeasure to request |
|---|---|---|---|
| Overproduction | Running unbooked colourways | Sudden discount offers on stock | Production released only against a PO |
| Waiting | Trim or fabric arriving late | Bulk start date slips a week | Material booking plan with dates |
| Transport | Panels moved between buildings | Long internal lead time | Cell layout for the style family |
| Over-processing | Tolerances the market ignores | High cost with no sales benefit | Spec review against channel standard |
| Inventory | Fabric bought in excess rolls | Old dye lots reappearing | Dye-lot control and roll tracking |
| Defects | Stitch and alignment rework | AQL 2.5 results near the limit | First-piece approval and defect Pareto |
| Motion | Operators fetching shared tools | Low minutes-per-unit improvement | Point-of-use tooling and jigs |
| Unused talent | Operator ideas never captured | Same problem recurring every run | Suggestion log with closed items |
The last row is the one buyers forget. A line that has run the same style for two years holds a great deal of practical knowledge about that style, and a supplier that captures it as standard work converts experience into yield. Ask to see the suggestion log and the closed items; it is a cheap and revealing request.
How Waste Shows Up in Your Quotation
Waste is priced into every quotation, even when the supplier does not call it that. A quotation built on 82 percent cut yield charges you for the 18 percent that becomes offcuts. One built on a heavily utilised line with frequent expediting charges you for the expediting. You cannot see these lines, but you can ask about them.
The practical approach is to request a cost breakdown at two quantity levels. If the per-unit drop between 500 and 2,000 pieces is larger than material economics alone would justify, part of the difference is set-up and waste recovery, and that part is negotiable once it is visible.
Necessary Waste Versus Pure Waste
Not all waste can be removed, and pretending otherwise produces bad decisions. Fabric offcuts from a shaped panel are largely unavoidable; some inventory is required as a buffer; some transport between buildings is structural. These are necessary but non-value-adding, and the goal is to minimise them, not to eliminate them.
Pure waste - waiting for a late trim item, reworking a mis-set seam, over-producing an unbooked colourway - has no justification and should be attacked first. Separating the two categories stops improvement effort being spent on things that cannot change.
Pull Scheduling Against a 35-50 Day Bulk Window
Push scheduling means producing to a forecast and then selling; pull scheduling means releasing work only when a real order draws it. For wholesale pet bags the practical version is a material booking plan tied to a confirmed purchase order. Fabric, webbing, zippers and packaging are booked against dates, and the cutting slot is reserved only when those dates are credible.
The buyer's role in a pull system is to make the order real early. A supplier cannot pull material against a verbal intention, and the difference between a deposit on day one and a deposit on day twenty is often the difference between a 35-day and a 50-day window. Buyers who complain about long lead times while holding approvals are usually looking at their own calendar, not the supplier's.
Pull also changes how capacity is allocated in peak season. When several customers compete for the same line slot, the supplier allocates to orders with released material and confirmed terms. Being early in that queue is a scheduling advantage that costs nothing but administrative discipline, and it is the single most reliable way to protect a seasonal launch date.
Set the plan in writing: material booking dates, cutting slot, packing slot, inspection date and ex-factory date, with a named owner for each. A plan with five dated milestones is far easier to manage than a single promised ship date, because slippage becomes visible while there is still time to react.
Takt Time, Line Balance and 500-Piece Lots
Takt time is the pace required to meet demand: available production time divided by required units. For a 500-piece lot on a line with a realistic daily output of 180-220 units, the sewing content fits inside two to three days. Everything else in the calendar is material, queue and set-up, which is precisely why small lots feel disproportionately expensive.
Line balance is the other half. If one workstation takes 90 seconds while the rest take 55, the line runs at the pace of the slowest station and the other operators wait. Rebalancing - moving one operation, adding a jig, or splitting a task - can lift daily output by 10-20 percent with no additional labour, and that gain is what makes shorter windows possible without overtime.
For buyers, the practical implication is to plan lot sizes around the line's natural rhythm rather than around an arbitrary round number. Two colourways of 500 run back-to-back on a balanced line often cost less per unit than one colourway of 1,000 split across two months, because the second arrangement pays the set-up twice and loses the continuity of the crew's learning curve.
Ask your supplier what the daily planned output is for your style and how many operators are assigned. Those two numbers let you sanity-check any promised window, and they expose quotations built on assumed overtime rather than on real capacity.
Why Line Balance Matters More Than Machine Count
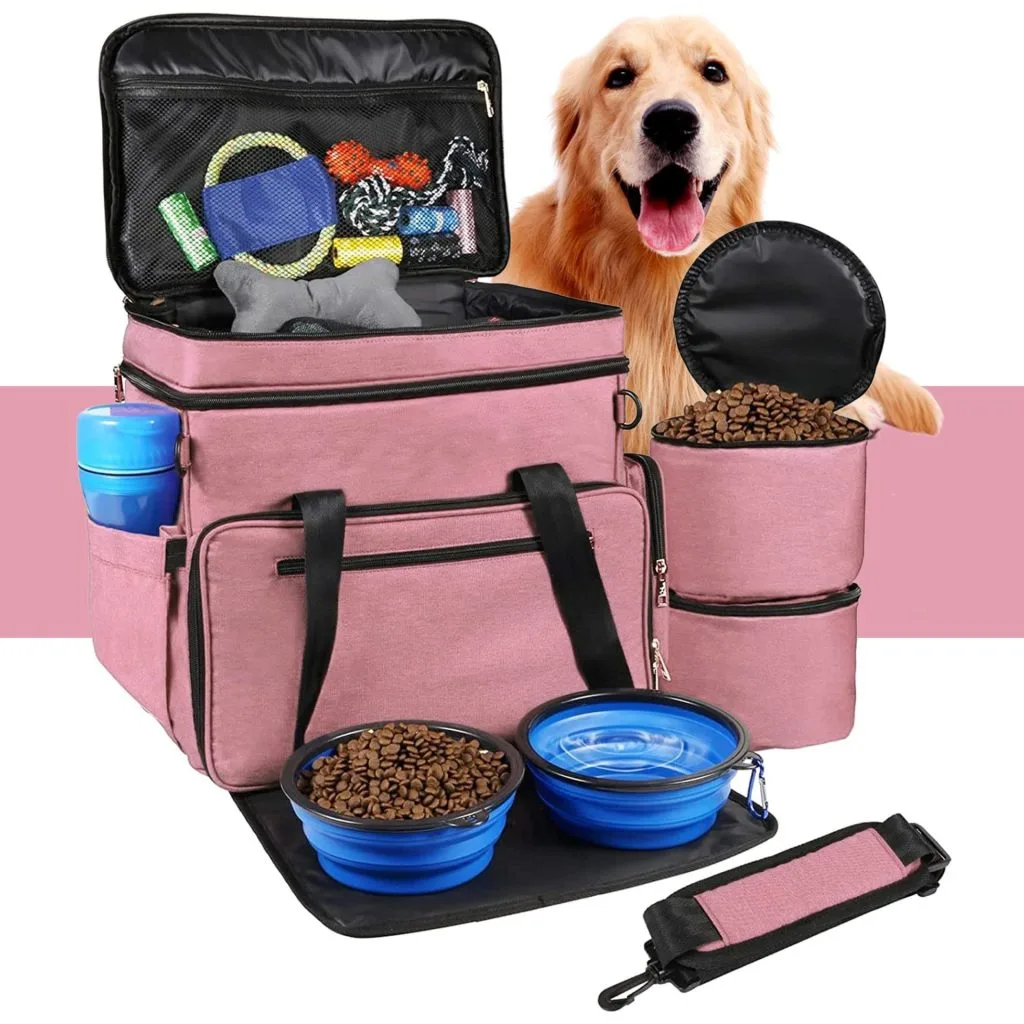
Buyers touring a facility often count machines as a proxy for capacity. Machine count tells you very little; balance and staffing tell you almost everything. A line of thirty machines staffed by eighteen operators produces at the pace of its slowest station regardless of how much equipment is idle beside it, and the binding constraint is usually one operation - setting a curved zipper, attaching a padded base board, or binding a mesh panel.
Ask which operation sets the pace for your style and how many operators are assigned to it. Those two questions identify the constraint, and the constraint is where any improvement effort should go. Adding capacity upstream of a bottleneck does nothing except build work in progress; adding it at the bottleneck raises output for the whole line.
There is a commercial angle too. When a supplier understands its own constraint, it can quote honestly about rush orders. A supplier that has never analysed balance will accept an expedite request it cannot fulfil, and you will discover the problem in week five rather than at booking.
Standard Work as the Basis for Any Quotation
Standard work documents the current best known method: the sequence of operations, the operator assignments, the standard minutes and the standard work-in-process quantity. It is the reference against which any quotation should be built, because it converts a price from an opinion into a calculation.
For buyers, the practical use is to ask whether standard minutes exist for your style and whether they have changed since the last order. If minutes are stable and material prices are stable, a price increase needs a specific explanation - a wage adjustment, a currency move, a material market shift. If no standard exists, pricing is negotiated rather than calculated, and it will move with sentiment.
Standard work also protects consistency between crews. Without it, two operators performing the same task in slightly different ways produce slightly different results, and the variation surfaces at final inspection as an unexplained defect cluster rather than as a process signal.
Value Stream Mapping From Fabric Roll to Carton
A value stream map traces one order from release to shipment and labels each step as value-adding, necessary but non-value-adding, or pure waste. In pet bag programs the map usually reveals that value-adding time is under 10 percent of total elapsed time, with the remainder in waiting and handling. That is not a criticism of any particular supplier; it is the normal state of cut-and-sew supply chains.
The map is useful to buyers because it identifies the two or three steps worth attacking. Common findings: fabric inspection happens after booking rather than at receipt, so a short roll is discovered mid-run; the sample approval loop runs sequentially instead of in parallel; and packing is specified after production, so cartons arrive late. Each finding maps to a fix with a date attached.
Requesting a map is a reasonable ask for any program above 1,000 pieces per year. It is a one-page document, it names the top three delays, and it gives both parties a shared list to work from. Suppliers running a genuine improvement program will already have one for their main style families.
Keep the map current. A map drawn once and filed is a snapshot; a map updated each season becomes the agenda for your business review, and it prevents the same three delays from being rediscovered every year.
Packaging, Cube and Freight Efficiency
Packing is where lean meets the freight invoice, and it is frequently the largest overlooked cost in wholesale pet bag programs. A bag that ships flat-packed with a removable base board can occupy 30-40 percent less cube than the same bag assembled with the board inserted. On a full container that difference is the difference between paying for air inside cartons and paying for product.
Carton right-sizing is the second lever. Standard cartons are often chosen from stock rather than designed for the product, leaving headroom that is then filled with void material. Designing the carton around the packed bag, and confirming the units-per-carton count before the carton order is placed, typically removes 5-10 percent of cube with no change to the product.
Retail channels add constraints here. Some require a specific carton count, a specific barcode placement or a pallet pattern, and those constraints must be known before packing is planned, not after. Provide the channel's packing specification with the order, and treat any deviation as a change requiring approval.
Incoterms determine who captures the benefit. Under FOB terms the buyer owns freight from the port, so cube reduction accrues to the buyer; under a delivered term the supplier may benefit instead. Confirm which party is measuring cube and who owns the saving before investing engineering time in it.
Carton Specification Data to Request
Ask for five numbers before packing is planned: carton inner dimensions, units per carton, carton gross weight, cartons per pallet, and total cubic metres for the order. Five figures let you model freight accurately and compare suppliers on landed cost rather than on unit price alone.
Confirm the carton specification at sample stage rather than at packing stage. Changing it late is where delays originate, because cartons are usually ordered against a confirmed count and a change means a new purchase with its own lead time.
When a Flat-Pack Option Changes the Product
Flat packing saves cube but can alter the customer experience, particularly where a base board or an internal frame must be inserted by the end user. That is acceptable for e-commerce channels and less so for shelf retail, where a shopper expects the product to look complete.
Decide by channel rather than by cost alone, and test the packing method on a real shipment before committing. A cube saving that generates a measurable rise in returns is not a saving.
Lean Metrics a Buyer Should Request Monthly
Three metrics capture most of what a buyer needs: on-time-in-full by order, lead time variance in days, and work-in-progress level at the peak of the run. On-time-in-full is stricter than on-time because it also catches partial shipments, which are a common and expensive failure mode. Lead time variance matters more than average lead time, because a supplier with a 40-day average and a 15-day spread is harder to plan around than one with a 45-day average and a 3-day spread.
Add two supporting numbers. Schedule adherence at the cutting slot tells you whether the internal plan is credible. First-pass yield tells you how much capacity rework is consuming. Together they explain most schedule slips before the slip happens.
Ask for these as a one-page monthly scorecard with stable definitions. The value of a scorecard is comparability: if the definition of on-time changes each month, the trend is meaningless and the conversation reverts to anecdote.
Set thresholds in the supply agreement. A simple rule - if on-time-in-full falls below an agreed level for two consecutive months, the supplier presents a recovery plan - converts a metric into a management tool without creating an adversarial relationship.
Where Lean Meets Compliance and Testing
Lean and compliance are often treated as separate departments, but they share the same evidence base. A restricted-substance screening programme depends on knowing which fabric lot and which trim batch went into which order, and that traceability is exactly what a disciplined material booking system produces. Suppliers with weak material control cannot answer either question reliably.
Testing lead time is also a flow problem. If a buyer waits until bulk production is finished before commissioning tests, any failure becomes a shipment-level problem. Booking tests against the approved sample, or against the first-off bulk units, keeps the test on the critical path rather than after it, and it protects the 35-50 day window from a late surprise.
Documented management systems provide the framework for this. Align your requirements with the principles set out in ISO 9001 quality management, verify certificate scope and validity through an independent body such as SGS, and reference recognised test methods from AATCC when you specify colour fastness or abrasion performance.
The buyer's action is to consolidate requirements into one document per program: the specification, the test list with methods and limits, the packing specification and the labelling requirement. One controlled document per program is what makes both lean flow and compliance auditable.
Contracting for Continuous Flow: What to Put in Writing
Flow commitments only hold when they are written into the commercial terms. The first clause to add is a milestone plan: material booking date, production start, inspection date and ex-factory date, each with a named owner and a notification trigger if a milestone slips by more than three working days. Early notification is worth far more than a penalty, because it gives you time to rebook freight or adjust a launch.
The second clause is quantity flexibility within the calendar. If your supplier has genuinely reduced changeover time, negotiate the right to split a confirmed annual volume into smaller releases without a price penalty. That right is the commercial expression of a lean capability, and it is often more valuable than a discount.
The third is data. Specify the monthly scorecard, the inspection report at AQL 2.5, and access to the defect Pareto. These are standard requests in wholesale pet bag sourcing and cost the supplier nothing if the data already exists.
Close with a review rhythm. A quarterly business review that looks at the scorecard, the value stream map and the coming season's forecast keeps the relationship on process rather than on price. Programs that review process quarterly tend to renegotiate price less often, because the cost base is already moving in the right direction.
What to Do When a Lean Program Stalls
Lean programs usually stall for one of three reasons: the metrics stopped being reviewed, the improvement work moved to low-value areas, or the buyer stopped noticing. All three are recoverable, and the diagnosis is quick if you look at the scorecard rather than at the narrative.
If reviews stopped, restart with a shorter agenda. A fifteen-minute monthly call covering three numbers is more sustainable than a quarterly workshop that nobody has time to prepare for. If the work moved to low-value areas, refocus on the defect Pareto and the biggest queue. If the buyer stopped noticing, reintroduce a commercial consequence - a volume commitment, a reduced inspection frequency, or a longer planning horizon.
One caution: do not respond to a stall by adding initiatives. Stalled programs almost never need more projects; they need fewer projects with clearer ownership and a visible review date.
Building a Joint Flow Review With Your Supplier
A joint flow review is a short, recurring meeting in which both sides look at the same three numbers: on-time-in-full, lead time variance and the top defect category. It should be scheduled, not convened when something goes wrong, because its purpose is prevention rather than recovery.
Prepare by sending your own data a day in advance - receipts, returns and any channel feedback - so the supplier arrives with its records rather than with opinions. Comparing two independent data sets is what makes the review productive, and discrepancies between them are usually informative rather than contentious.
Close every review with two decisions and two dates. Anything more tends not to happen. Over two or three quarters, a disciplined review rhythm does more for cost and reliability than any single renegotiation.
Why brands source here
- Pet bag programmes run since 2014; founding team in sewn goods since 2004
- SGS-verified production floor of 4,950 m² with 137 workers across 7 lines
- Monthly capacity of 200,000 units, audited to BSCI and ISO 9001
People Also Ask
What is the difference between lean and kaizen?
Lean is the overall system for removing waste and managing flow; kaizen is the daily improvement activity that feeds it. A supplier can run kaizen events without a lean system, but the gains rarely hold.
Why do small pet bag orders feel disproportionately expensive?
Set-up and changeover consume line capacity that is not recovered at 500 pieces. Reducing changeover time is what makes small lots economically sensible.
What is takt time in simple terms?
It is the pace needed to meet demand: available production time divided by units required. Comparing takt time with actual daily output shows whether a promised window is realistic.
How do I measure a supplier's schedule reliability?
Track lead time variance in days across the last six orders, plus on-time-in-full. Low variance matters more than a short average because planning depends on predictability.
Should packing be specified before or after production?
Before. Carton design, units per carton and barcode placement must be known when the packing slot is booked, or cartons arrive late and hold the shipment.
How much cube can flat packing save?
Typically 30-40 percent for styles with a removable base board, which on a full container is a significant landed-cost reduction for an identical product.
What should a supply agreement say about delays?
Specify dated milestones with a notification trigger, usually a three-working-day slip. Early notice lets you rebook freight and protect a launch date.
Frequently Asked Questions
What does lean manufacturing mean for a pet bag buyer?
It means the supplier manages flow, not just output: material is booked against a released plan, work is levelled across the calendar, and waste such as waiting and rework is measured and reduced. The buyer sees it as a shorter, more predictable bulk window.
How much can lean reduce a pet bag production lead time?
Realistic gains are 8-15 percent of the production calendar, mostly from removing queue time rather than sewing faster. On a 35-50 day window that is typically three to seven days.
Does lean change the MOQ of 500 pieces?
Not the stated minimum, but it lowers the cost penalty of running at that size. Faster changeovers and balanced lines make repeated 500-piece releases more economical than they would be on an unbalanced line.
What is on-time-in-full and why is it better than on-time?
It measures whether the full quantity arrived on the promised date. Partial shipments pass an on-time measure but still disrupt a launch, so on-time-in-full is the stricter and more useful metric.
How do I check whether a supplier really runs lean?
Request a value stream map for your style family, a monthly scorecard with three months of history, and the current work-in-progress level. Documented answers indicate practice; vague assurances indicate otherwise.
Where is the biggest hidden waste in pet bag orders?
Usually waiting for trim and packaging materials, followed by packing cube that was never engineered. Both are cheap to fix and both are invisible in the unit price.
How does packing cube affect my landed cost?
Cube determines how many units fit a container, so it divides freight across more or fewer units. A 10 percent cube reduction on a full container is a direct landed-cost saving with no product change.
Should I press for a shorter bulk window?
Only if your own approvals are fast. A large share of schedule loss happens on the buyer side, so compressing the supplier's window while holding approvals for days yields nothing.
How does lean interact with AQL 2.5 inspection?
Lean reduces the defect rate that inspection samples; inspection verifies it. Relying on the gate alone leaves rework capacity consumed, which is itself a cause of late shipments.
Is a value stream map a reasonable request from a buyer?
Yes, particularly for programs above 1,000 pieces a year. It is a one-page document naming the top delays, and suppliers with a real improvement program usually maintain one already.
What Incoterm should I use to capture freight savings?
Under FOB terms the buyer controls and pays freight from the port, so cube reductions accrue to the buyer directly. Confirm the term before investing in packaging engineering work.
Can lean work on seasonal, low-repeat styles?
Partly. Flow discipline always helps, but the large gains come from repeat styles where standard work and jigs can be amortised. Seasonal one-offs benefit mainly from better material booking.
Talk to QUANZHOU JUNYUAN BAGS about a wholesale pet bag order: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample